Pharma Conveyors
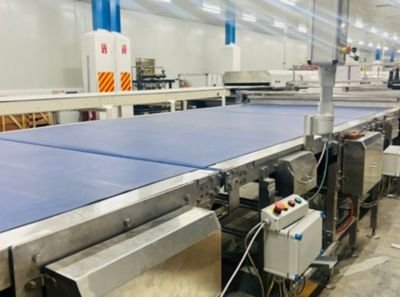
Our pharmaceutical conveyors are specifically engineered to meet the stringent hygiene and safety standards of the pharmaceutical industry. Constructed using corrosion-resistant stainless steel, food-grade plastics, and sanitary belts, these conveyors are designed to ensure the contamination-free handling of products while maintaining optimal performance. Operating at speeds between 0 and 80 meter per minute, these conveyors are customized to suit the demands of pharmaceutical production processes.
Key features of Pharma Conveyors
- Corrosion-Resistant Stainless Steel Construction: Provides durability and easy cleaning, essential for maintaining hygiene in pharmaceutical environments.
- FDA-Approved Food-Grade Plastics: Made from non-reactive materials such as polypropylene (PP) or polyethylene (PE), ensuring product safety and compliance with industry regulations.
- Sanitary Belts: Equipped with FDA-approved polyurethane (PU) or silicone belts that are easy to sanitize and designed to prevent bacterial growth, ensuring safe product handling.
- Tailored Operating Speeds: Runs at speeds ranging from 0 and 80 meter per minute, providing flexibility to match the specific requirements of pharmaceutical production lines.
- Hygienic Design: Smooth, non-porous surfaces and easy-to-clean components help minimize contamination risks, ensuring safe and efficient product transport.
Critical Parts of a Pharmaceutical Conveyor
Our pharmaceutical conveyors are built with top-quality components from industry-leading manufacturers, ensuring reliable performance and strict adherence to pharmaceutical safety standards:
- Conveyor Belt (Sanitary and Food-Grade Belts)
- Manufacturers: Habasit, Chiorino,Ammeraal Beltech, Forbo Siegling, and local FDA-approved belt suppliers
- Purpose: Provides smooth, contamination-free transport of pharmaceutical products, with easy-to-clean surfaces that support sanitation protocols.
- Drive Motor and Gearbox (Power and Speed Control)
- Manufacturers: SEW Eurodrive, Nord Drivesystems, Bonfiglioli
- Purpose: Delivers consistent power with precise speed control to ensure smooth operation and flexibility to meet the specific needs of production processes.
- Stainless Steel Frame (Corrosion-Resistant and Easy to Clean)
- Purpose: Ensures the structural integrity of the conveyor while being easy to clean and resistant to the corrosion caused by cleaning agents and high-humidity environments.
- Bearings and Pulleys (Smooth Operation and Belt Support)
- Manufacturers: SKF, Timken, Dodge (Baldor)
- Purpose: Facilitates smooth belt movement and supports high-precision product transport, reducing downtime and wear.
- Sensors and Controls (Automation and Monitoring)
- Manufacturers: Siemens, Omron,Sick Sensor’s, Allen-Bradley (Rockwell Automation)
- Purpose: Offers real-time monitoring and automation for seamless integration with production lines, enhancing productivity and ensuring strict control over product flow.
- Conveyor Belt (Sanitary and Food-Grade Belts)
Standard Features
- Stainless steel frame for superior corrosion resistance and hygiene.
- FDA-approved PU or silicone belts designed for easy cleaning and sanitation.
- Variable operating speeds from 0 to 80 meter per minute to accommodate different production needs.
- Hygienic design with removable parts for easy cleaning and maintenance.
Optional Features
- Customized conveyor designs to fit specific production requirements.
- Enhanced automation systems for real-time monitoring and speed adjustment.
- Clean-in-place (CIP) systems for automated cleaning, reducing downtime and manual intervention.
- Enclosed conveyor options to protect products from external contaminants.
- Anti-static features for sensitive pharmaceutical products, ensuring safe handling in controlled environments.
Elevate Your Productivity with NV-GEN Pharma Conveyors
Our pharmaceutical conveyors are designed to meet the highest standards of hygiene, safety, and efficiency in the production of medicines, supplements, and other healthcare products. By using only the best materials and components, our conveyors ensure safe and reliable transport, helping manufacturers maintain compliance with stringent pharmaceutical regulations.